
Smart glasses manufacturer or trading company? The 15-point test
In consumer electronics the line is deliberately blurred: trading companies register factories on video, factories run export front companies, and both quote similar brochures. This page gives sourcing teams the evidence-based checks that separate a real production site — with tooling, lines and engineering — from a reseller adding margin and risk between you and the floor.
Two business models, two risk profiles
Trading companies are not always dishonest — but they cannot control what they do not own: the line schedule, the BOM, the test lab submission or the change history behind your certificate.
Direct manufacturer
Owns or directly operates the production assets and engineering that create the product. CYNRIN programs are quoted and run this way.
- SMT and assembly lines, tooling and fixtures are its own assets on its floor
- Engineering signs the BOM, test plans and certifications; labs talk to its engineers
- Certificates can be filed in your brand name against the actual manufacturing site
- Price contains one organization's overhead; reorder and change control are direct
- Quality records, lot traceability and corrective actions come from the source
- NRE, tooling and line slots can be demonstrated, not just described
See what that looks like on the Shenzhen factory page and the R&D stage-gate process.
Trading / intermediary company
Buys from one or more factories and resells to export buyers. Often valuable for fragmented, low-tech categories — problematic for certified electronics.
- No owned lines or tooling: capacity claims depend on unnamed third parties
- Engineering questions are relayed, delaying the answers a launch depends on
- Certificates often belong to another entity; brand-owned filings may be impossible
- Price includes intermediary margin layered over the factory price
- Quality enforcement stops at the trader's salesperson, not the production floor
- Factory changes behind the scenes can silently invalidate certifications and samples
Traders can still be the right partner for unbranded commodity stock; they are a structural risk for a certified, brand-owned eyewear program.
Evidence a real manufacturer can produce without hesitation
Run this list during vendor qualification. Weight the documentation checks heavily — video tours can be borrowed; certificate chains and engineering depth cannot.
Business license scope
License scope includes manufacturing/production (not only trading, import-export or technology consulting); registered address plausibly matches the factory site.
Site address consistency
Company, factory, quotation bank details and shipping origin all point to related entities at consistent addresses — not an office tower for a claimed 500-worker plant.
Live facility walk
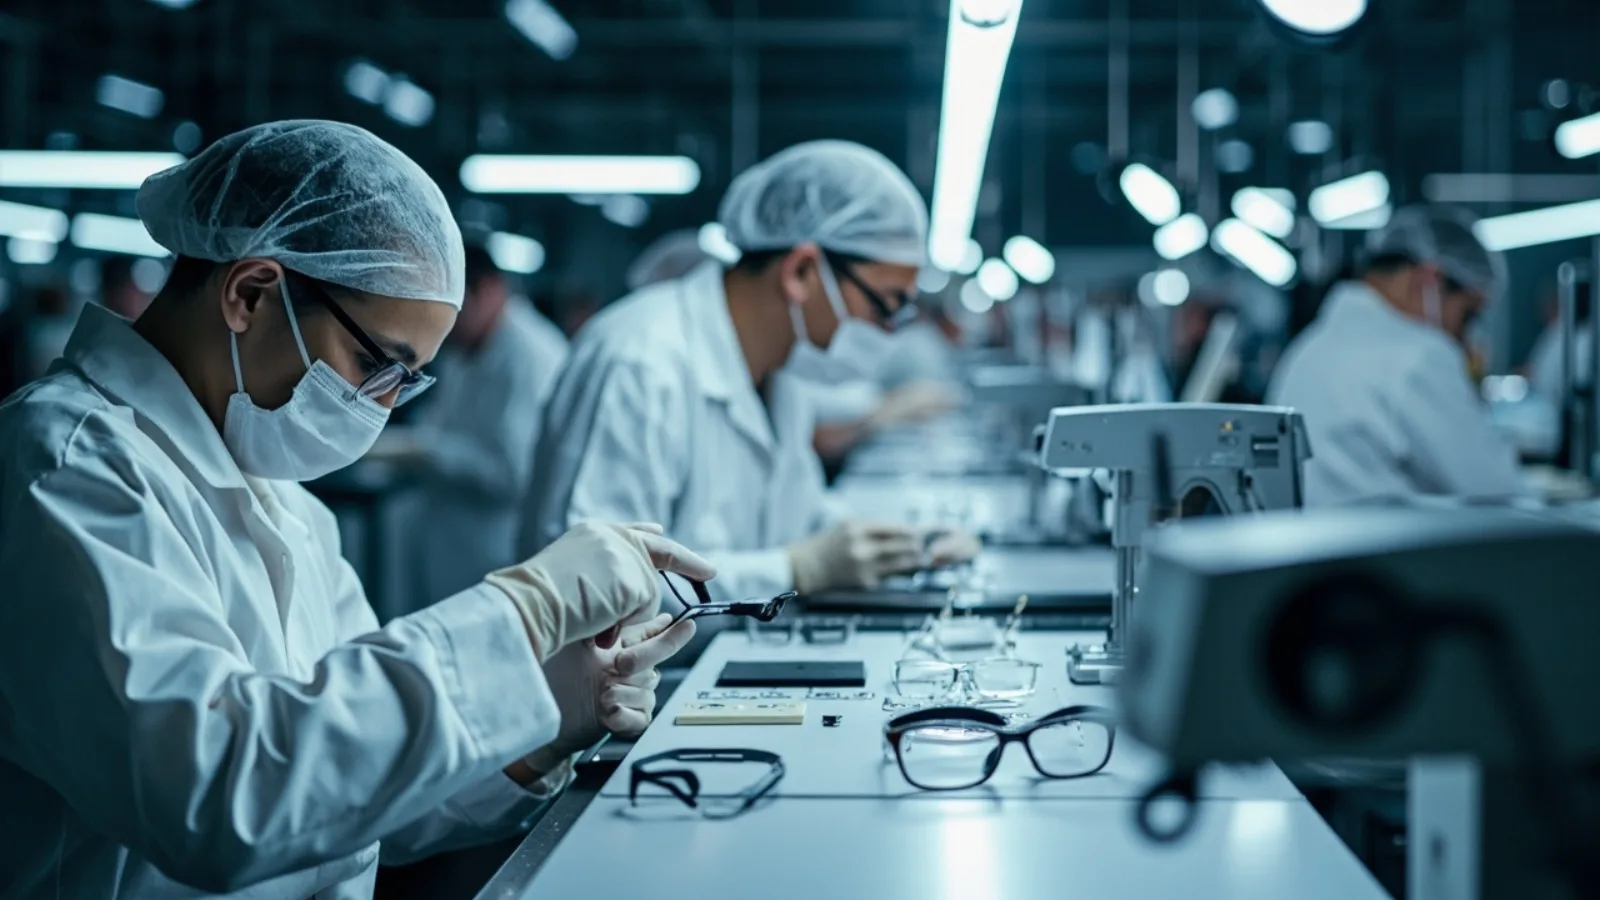
Unscripted video call at a requested time showing SMT, assembly, aging and warehouse, with current date evidence and ability to ask for specific machines.
SMT line evidence
Pick-and-place, reflow, AOI/spi and PCBA handling on site, running boards of the product family — eyewear or comparable compact electronics.
Tooling ownership
Ability to show molds/fixtures, tooling invoices or mold-flow records for custom programs; willingness to write tooling ownership into the contract.
BOM transparency
Component-level BOM with approved vendor list for the key parts — SoC, module, sensor, battery, hinge, lens — not a vague "high quality materials" sheet.
Battery cell traceability
Named cell supplier with matching UN38.3 summary and MSDS; ability to lock the cell in the BOM at PVT (see the battery file).
Certificate chain
Test reports and certificates identify the actual factory/manufacturer entity; willingness to file new certificates in your brand name, not only lend expired third-party PDFs.
Engineering access
Direct technical dialogue with RF, mechanical and firmware engineers before order — a trader's relay pattern is obvious inside two technical questions.
Quality system records
IQC/IPQC/OQC procedures, AQL standards and sample record forms; a real lot of failure-analysis or corrective-action documentation shown on request.
Calibration & lab
RF/pre-scan, reliability and measurement equipment with calibration labels and current dates — not decorative instruments in a showroom.
Sample-to-mass consistency
Written commitment that certification samples come from the PVT pilot build and match mass production — the core promise behind certification handling.
Contract depth
Contract covers tooling ownership, BOM lock, change notification, IP, inspection criteria and penalty/recall terms; traders resist specificity on production obligations.
Financial plumbing
Bank account beneficiary matches the contracted manufacturer; willingness to use transparent milestone deposits per the payment structure, not only full prepayment to a personal-style entity.
Reference reality
References are verifiable customers or observable evidence of export history; showroom walls of anonymous logos are marketing, not verification.
Red flags during the first ten emails
Every product, every spec
A catalog spanning unrelated categories with identical enthusiasm signals aggregation, not production depth in smart glasses.
No technical answers
Questions about antenna, SoC, EN 18031 or test routes bounce back as "no problem, we can do" with no engineering substance.
Borrowed certificates
Offered certificates name a different company and address, with refusal to file new ones in your brand or explain the licensing chain.
Live tour avoidance
Repeated excuses for an unscripted facility call, or a "factory" that is never producing your product family during visits.
Price that beats the BOM
Quotes materially below plausible component cost usually mean unannounced part substitution after deposit — the classic trader squeeze.
Full prepayment pressure
Insistence on 100% upfront with no milestone linkage to samples, tooling or inspection, and beneficiary mismatch concerns.
Golden-sample vagueness
No sealed-sample process, no written production standard, and resistance to AQL inspection clauses.
Address rotation
Office, claimed factory, invoicing entity and shipment origin in multiple names with no explainable group structure.
What to do with four hours on site
Hour 1 · Floor reality
Walk SMT to packaging unguided enough to see WIP labels and boards; confirm the product family is physically in production, not staged.
Hour 2 · Evidence room
Ask to see calibration records, a current BOM, one lot's inspection forms and the actual UN38.3 summary for a shipping cell.
Hour 3 · Engineer time
Sit with RF/mechanical/firmware engineers on certification routing and your specific architecture; note who can answer without relaying.
Hour 4 · Commercial checks
Match license, facility lease/ownership, bank beneficiary and tooling records; agree the sealed-sample and inspection process there and then.
Can't travel? A remote audit on the same checklist, plus a third-party inspection at the standard quality gates, closes most of the gap before deposit.
Sourcing questions about factories and traders
Is a trading company ever the right choice for smart glasses?
Can a trading company hold the certifications and let us use them?
What does a manufacturer's quotation look like versus a trader's?
How do I verify the factory without visiting China?
The factory says certificates cost extra and take weeks after deposit — normal?
How does CYNRIN answer this checklist?
12-point manufacturer selection guide
The full evaluation framework for choosing an eyewear OEM partner.
Read 02Facility & lines
What the Shenzhen site operates and what an audit sees.
Explore 03Supplier quality questions
The email-ready audit script behind this 15-point checklist.
Read 04Run the checklist on us
Request the evidence pack, live tour and engineer call for your program.
StartCompare vendors on evidence, not brochures.
Send the checklist in your RFQ. CYNRIN returns the document pack, BOM detail and a standing invitation to the live facility walkthrough.